We are glad to share with you about the results of our work, company news,and give you timely developments and personnel appointment and removal conditions.
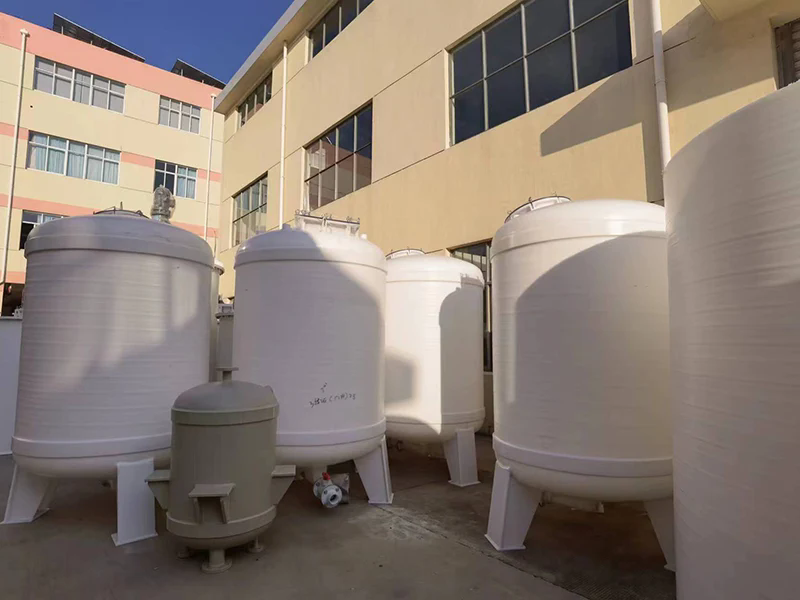
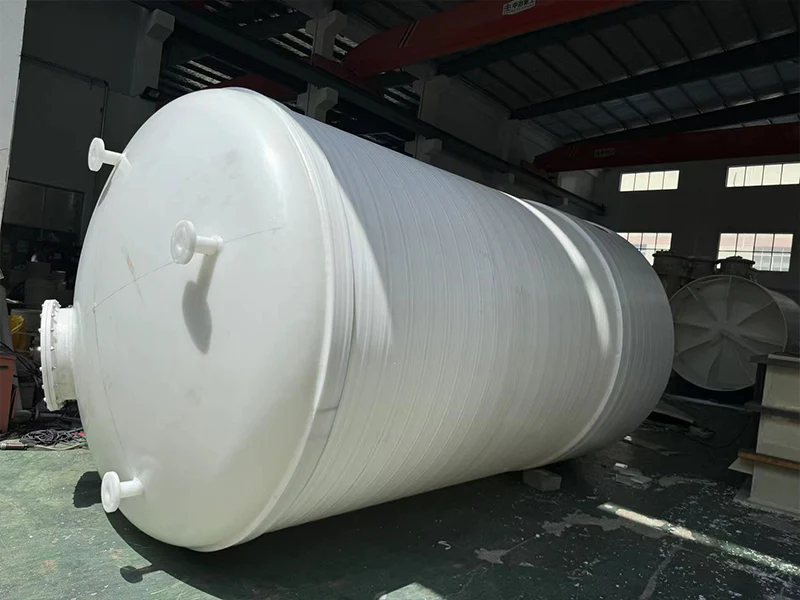
Polypropylene storage tanks have become a cornerstone in industrial, chemical, and agricultural sectors due to their durability, chemical resistance, and cost-efficiency. Designed to store a wide range of liquids, including corrosive chemicals and potable water, these tanks combine reliability with environmental adaptability.
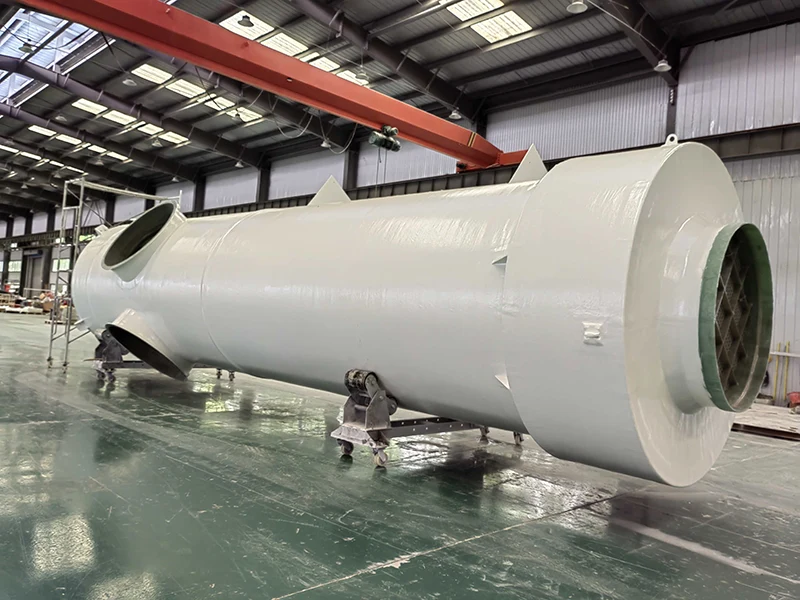
FRP Equipment is widely used in chemical processing, water treatment, and high-corrosion industrial lines due to its lightweight stability and enhanced resistance to aggressive chemicals.
Polypropylene Vacuum Filter has emerged as a critical solution across chemical processing, pharmaceutical manufacturing, wastewater treatment, laboratory filtration, and food-grade separation. Engineered from highly resistant polypropylene, this filtration system delivers strong chemical stability, long service life, and low maintenance requirements.
PP Composite FRP Equipment provides a combination of corrosion resistance, mechanical stability, lightweight construction, and cost efficiency that traditional systems often cannot match.
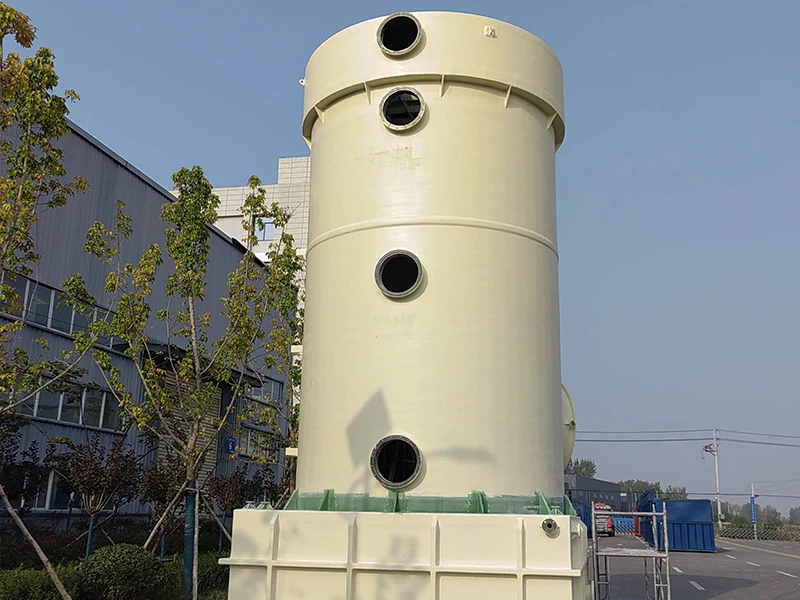
Across chemical processing, gas purification, wastewater treatment, and mass-transfer operations, the demand for corrosion-resistant, lightweight, and cost-effective tower equipment continues to rise. Among the available materials, Polypropylene (PP) Packing Towers have gained widespread adoption due to their excellent chemical resistance, stable hydrodynamic performance, and compatibility with various structured and random packing materials.
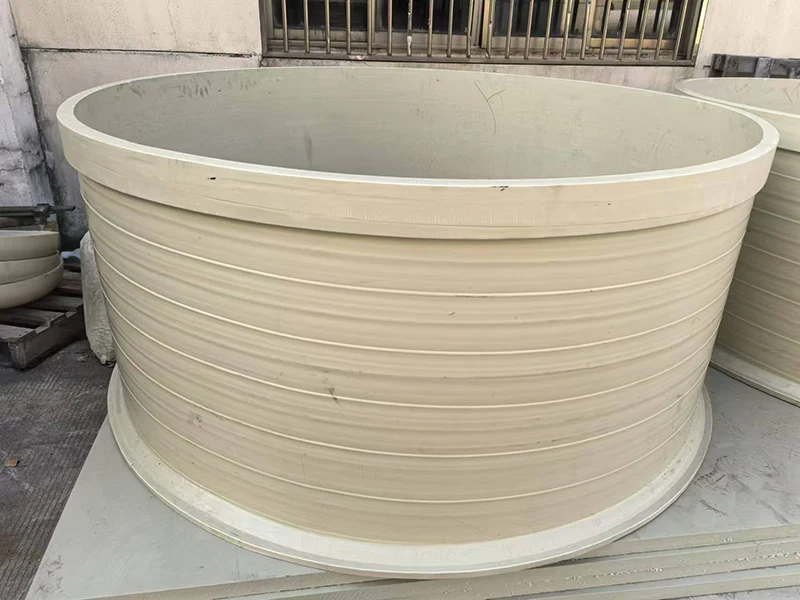
PP Composite FRP Equipment is increasingly favored in modern chemical and industrial applications due to its superior corrosion resistance, lightweight structure, and durability.
We use cookies to offer you a better browsing experience, analyze site traffic and personalize content. By using this site, you agree to our use of cookies. Privacy Policy
 08 2025-12
 05 2025-12
 01 2025-12
 28 2025-11
 24 2025-11
 20 2025-11